
Established in 2014, SIBLINETEK is Sibline’s Building Materials business, delivering high-quality precast concrete solutions for modern construction and outdoor development. Our portfolio includes regular and lightweight hollow blocks, pavers, curbstones, segmental retaining wall blocks and other precast concrete solutions, serving structural, architectural, landscaping and infrastructure applications.
ENGINEERED FOR PERFORMANCE
SIBLINETEK products are manufactured using carefully selected materials, optimized concrete mixes and controlled production processes to meet the requirements of different applications. Our concrete blocks offer a range of densities from 1,000 to 2,200 kg/m³, providing solutions adapted to different project needs. Manufactured in a technologically advanced facility and supported by dedicated laboratory testing and quality control, our products are developed to deliver reliable performance, durability and ease of application in accordance with applicable standards.
CUSTOMER SUPPORT
Our commitment extends beyond manufacturing. A specialized team of engineers and technical professionals supports customers, contractors and project stakeholders throughout the product selection and application process. From understanding project requirements to selecting the appropriate solution, we provide practical technical guidance and project support to help achieve the right result.
The Building Blocks Laboratory is a strategic quality assurance unit within our manufacturing facility. It plays a critical role in ensuring that all raw materials and finished concrete masonry units (CMUs) comply with international standards and meet the highest levels of performance, durability, and safety.
Operating with advanced testing equipment and qualified technical personnel, the laboratory supports production, R&D, and continuous improvement initiatives across the plant.
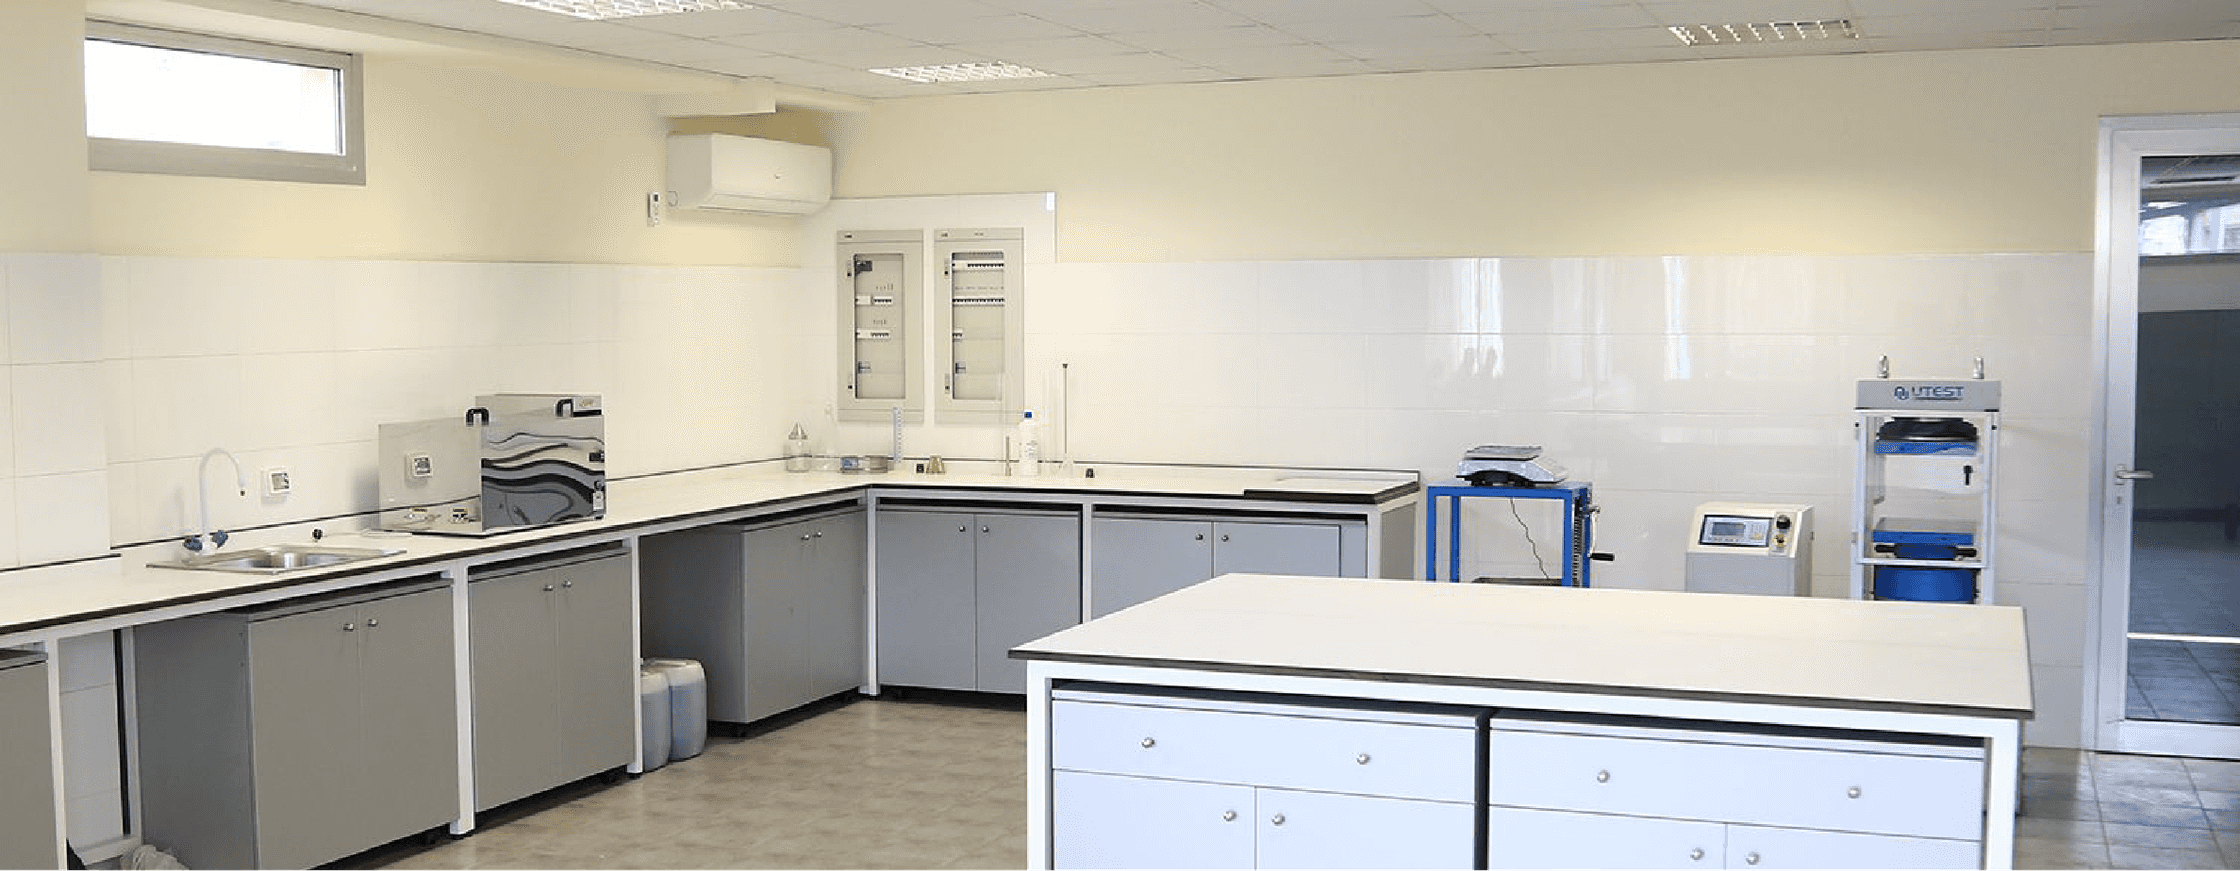
The laboratory ensures:
• Strict compliance with international standards
• Continuous monitoring of raw material quality
• Performance validation of finished products
• Process optimization through data-driven control
• Technical support for clients and regulatory bodies
Our objective is to guarantee consistency, reliability, and long-term durability of our building blocks in all applications.
Quality starts before production. Our laboratory controls and tests key raw materials, including aggregates, cement, water and applicable admixtures, in accordance with relevant ASTM requirements. Combined with controlled batching, production monitoring and regular sampling, these processes ensure consistent materials and production quality.
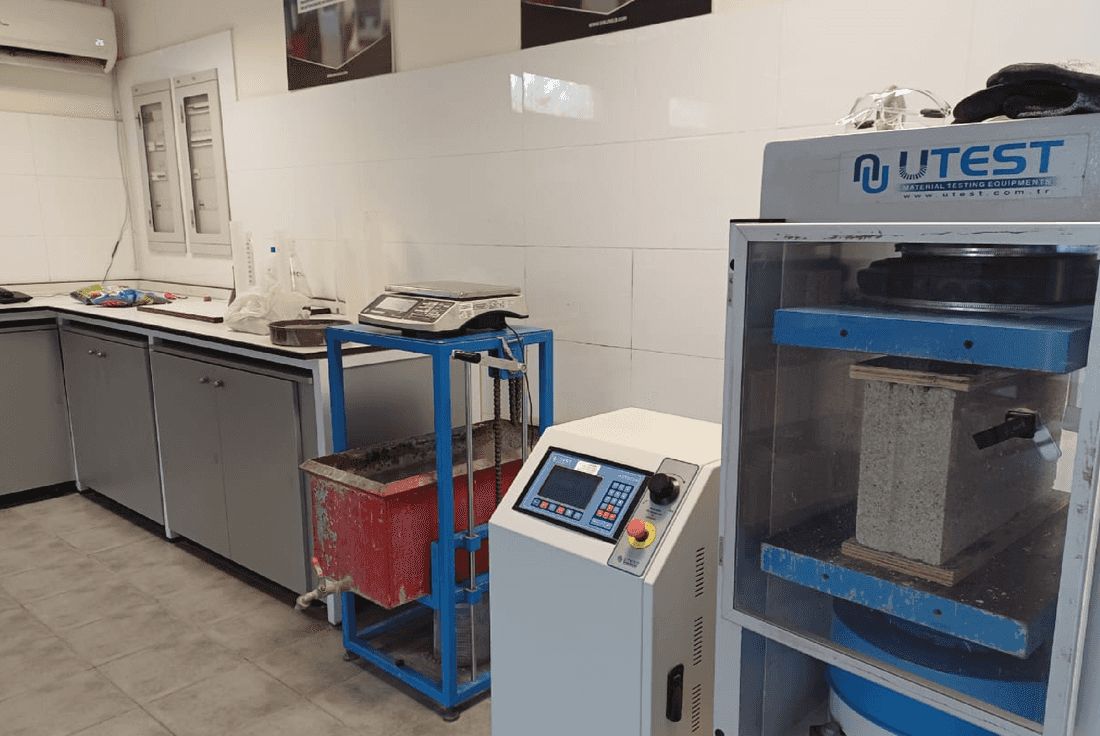
Finished building blocks are systematically tested in accordance with the applicable requirements of EN 771-3 for aggregate concrete masonry units. Key performance characteristics such as compressive strength, density, dimensions and water absorption are verified to ensure that products meet their defined specifications and intended performance.
Our laboratory supports customer and project requirements through technical evaluation, sample testing and compliance support when required. Testing is backed by traceability, calibrated equipment and documented results, providing reliable technical information for quality assurance and continuous improvement. Technical data sheets, product specifications and relevant test or conformity documents are available for consultation.
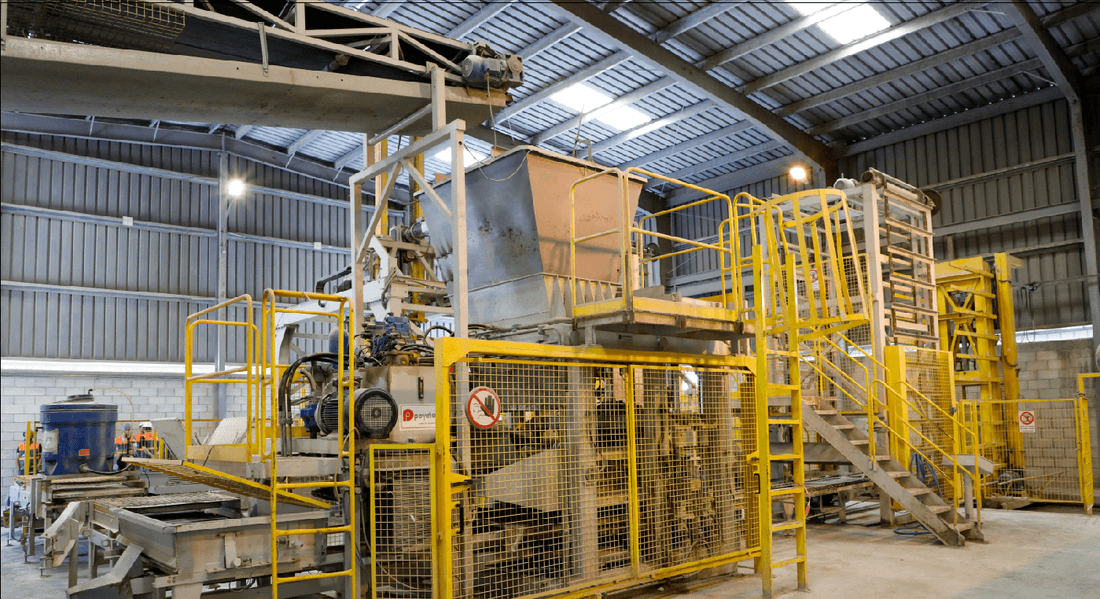
The Building Blocks Laboratory is more than a testing facility — it is a cornerstone of our quality commitment. Through rigorous control of raw materials and finished products, we ensure that every block delivered to the market meets international standards and customer expectations.